
Description
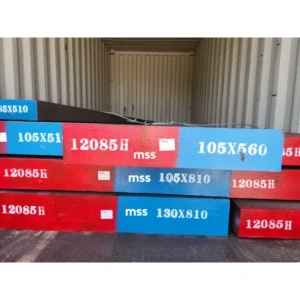
Buy DIN 1.2085 Steel (DIN X33CrS16, AISI 420FM, and BÖHLER M315) it’s a stainless plastic mold steel in plates & rounds at the best price in India.
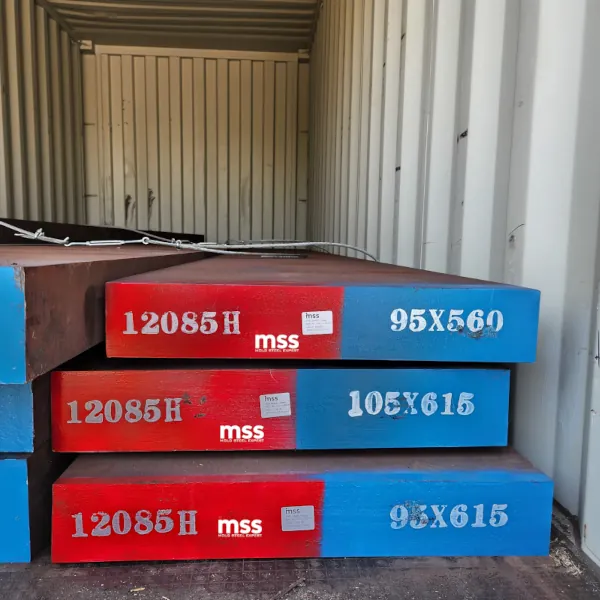
Milano Special Steel supplies DIN 1.2085 steel, also known as DIN X33CrS16, AISI 420FM, and BÖHLER M315, for plastic mold and die applications across India in plates and rounds, with fast delivery and reliable quality. This free-machining, corrosion-resistant martensitic stainless steel is engineered for plastic mold bases, frames, ejector plates, and general mold tooling that demands good machinability, consistent hardness (typically prehardened), and resistance to corrosive molding environments.
As one of India’s leading importers, processors, and suppliers, we stock 1.2085 in both standard and customized sizes, supporting both wholesale and retail orders, and offer a cut-to-size service. With over 50 years of experience since 1972, we serve manufacturing hubs in Gurugram, Kundli, Sonipat, Manesar, Bawal, Bhiwadi, Dharuhera, Faridabad, Ghaziabad, Noida, and Greater Noida, and deliver to all Indian states and union territories.
DIN 1.2085 Steel Key Equivalents and Designations
-
DIN/W.-Nr.: 1.2085
-
EN designation: X33CrS16
-
AISI/ASTM: 420FM (free-machining 420-type mold steel)
-
Brand equivalents: BÖHLER M315 and comparable free-machining 420 mold steel grades from major European and Japanese mills
-
Typical supply conditions: Annealed (for further heat treatment), prehardened (most common for mold bases)
What Makes DIN 1.2085 Steel Unique?
-
Free-machining stainless tool steel with elevated sulfur for improved machinability.
-
Chromium content around 15–16% provides strong corrosion resistance in humid environments and against inevitable acidic plastic by-products (e.g., PVC, flame-retarded polymers).
-
Stable pre-hardened hardness with reasonable dimensional control during machining and finishing.
-
Ideal for high-volume mold base components where machining speed, stable hardness, and corrosion resistance matter more than ultra-high polish or maximum toughness.
Why Milano Special Steel
-
Top importer and national distributor of premium European and Asian mill material.
-
Dependable stock in plates and rounds, with traceability and mill test certificates (MTC).
-
Precision sawing, facing, rough milling, grinding, and heat-treatment support.
-
Fast cut-to-size service for both single pieces and bulk lots.
-
Pan-India delivery network and dedicated technical assistance for grade selection.
DIN 1.2085 Steel Typical Chemical Composition
The following values are nominal/typical ranges for DIN 1.2085 Steel (X33CrS16, AISI 420FM):
-
C: 0.28–0.38%
-
Cr: 15.0–16.5%
-
S: 0.10–0.20% (free-machining addition)
-
Mn: 0.50–1.20%
-
Si: 0.20–1.00%
-
P: ≤ 0.03%
-
Mo: 0–0.60% (presence depends on mill variant)
Note: Individual mill specifications may vary slightly; always refer to the MTC for exact chemistry.
DIN 1.2085 Steel Mechanical Properties and Hardness
-
Supply hardness (prehardened): typically 28–34 HRC, with standard ranges around 30–33 HRC for mold base use.
-
Tensile strength (typical, prehardened range): approximately 1,000–1,200 MPa.
-
Yield strength (typical, prehardened range): approximately 800–1,000 MPa.
-
Impact toughness: adequate for mold base and plate applications; for highly stressed inserts, consider tougher grades.
-
Dimensional stability: good in pre-hardened condition with controlled heat input during machining/welding.
Values are indicative and depend on section size, heat-treatment condition, and mill practice.
DIN 1.2085 Steel Supply Forms, Sizes, and Processing
-
Forms: Plates, rounds, blocks, flat bars, and near-net pre-machined blocks on request.
-
Thickness/diameter range: From small rounds and thin plates up to large blocks for sizable mold bases.
-
Cut-to-size: High-accuracy band-saw cutting for single or multiple pieces with tight length tolerances.
-
Processing services:
-
Rough milling and face milling for setup-ready plates
-
Grinding to thickness or parallelism as required
-
Drilling and tapping on request (for standard patterns)
-
Normalizing/tempering guidance and heat-treatment coordination
-
Surface conditioning and rust-preventive packaging
-
DIN 1.2085 Steel Applications
-
Plastic mold bases and frames for injection molding and compression molding
-
Ejector plates, support plates, spacer blocks, and backing plates
-
Mold components for corrosive plastics: PVC, flame-retarded materials, and plastics with aggressive additives
-
Trim tools and general tooling plates where stainless properties and easy machining are beneficial
-
Aluminum and pressure die casting tooling housings, fixtures, and plates that benefit from corrosion resistance and stable pre-hardened hardness
-
Jigs, fixtures, and machine components in humid or corrosive shop environments
For high-thermal-shock die inserts or hot-working cores, consider alternative hot-work grades (e.g., H13/1.2344 ESR). Use 1.2085 primarily for mold bases and plate components in those setups.
DIN 1.2085 Steel vs Related Tool Steels
| Property/Use Case | 1.2085 (X33CrS16, 420FM) | 1.2083 (X40Cr14, AISI 420) | 1.2316 (X38CrMo16-1) | P20 (1.2311/1.2312) | H13 (1.2344) |
|---|---|---|---|---|---|
| Corrosion resistance | High (Cr ~16%, S added) | High (Cr ~13–14%, better polishability) | Very high (Cr ~16–17%, Mo alloyed) | Moderate | Moderate |
| Machinability | Very good (free-machining) | Moderate | Moderate | Good | Moderate |
| Pre-hardened typical HRC | 28–34 | 28–32 | 28–34 | 28–34 | 38–45 (hot work) |
| Polishability (mirror) | Moderate (S limits top-tier mirror) | Very good (preferred for high-gloss) | Good–very good | Moderate | Moderate |
| Hot strength | Low (not for hot inserts) | Low | Low | Low–moderate | High (hot work) |
| Typical use | Mold bases, plates | Mirror-finish cavities | Corrosion-critical molds | General mold steel | Hot work dies/inserts |
Guidance:
-
Choose DIN 1.2085 Steel if you want stainless resistance plus fast machining for bases/plates.
-
Choose 1.2083 for high-gloss mirror cavities.
-
Select 1.2316 for maximum corrosion resistance and improved toughness in cavity components.
-
Choose P20 for general plastic molds where corrosion is manageable.
-
Choose H13 for hot-work or die-casting inserts.
Heat Treatment Guidelines
-
Annealing (Softening)
-
Heat to approximately 740–800°C.
-
Slow cool in the furnace at ≤10°C/hour to about 600°C, then air cool to room temperature.
-
Result: ~HB 200–230 (varies with section size).
-
Stress Relieving
-
After heavy machining, heat to ~600–650°C.
-
Hold 1–2 hours, depending on the section.
-
Cool in still air.
-
Helps minimize distortion during subsequent finishing.
-
Hardening
-
Austenitizing: ~980–1,050°C (check mill datasheet for exact target range).
-
Quench: air, oil, or polymer, depending on section thickness and required distortion control.
-
Temper immediately after reaching hand-warm temperature.
-
Tempering
-
Temper at 180–300°C based on target hardness and service requirements.
-
Typical tempered hardness range: 48–52 HRC is possible on hardening grades; however, many customers use the grade pre-hardened at ~30–33 HRC for mold bases.
-
Multiple tempers recommended for dimensional stability.
Notes:
-
Elevated sulfur improves machining but slightly reduces toughness and enhances very high gloss polishability.
-
For optimal polishing performance, adhere to meticulous finishing protocols and consider 1.2083 or 1.2316 for mirror-critical surfaces.
Machining, EDM, Grinding, and Polishing
-
Machining: DIN 1.2085 Steel machines quickly due to sulfur content; use sharp tools, optimized cutting speeds, and proper coolant to evacuate chips.
-
EDM: Use stable parameters, minimize recast layer, and always perform post-EDM stress-relief or light polish where surface integrity is critical.
-
Grinding: Avoid excessive heat; dress wheels appropriately and use coolant to prevent burn and residual stresses.
-
Polishing: Capable of fine finishes on bases and plates. For optical/mirror-grade cavity finishes, 1.2083 typically outperforms due to lower sulfur and higher purity.
Corrosion Resistance and Surface Treatments
-
Intrinsic stainless behavior with Cr ~16% provides good resistance to humidity, sweating molds, and certain corrosive plastic by-products.
-
For enhanced surface performance, consider:
-
Nitriding (controlled, low-temperature processes compatible with stainless)
-
PVD coatings (e.g., TiN, TiCN, DLC) for wear control on specific components
-
Passivation to maximize corrosion resistance post-machining and post-welding
-
Proper maintenance (cleaning, drying, and rust-preventive oils during storage) preserves surface integrity and dimensional stability.
Welding
-
Weldable with matching or compatible stainless tool steel fillers.
-
Preheat: commonly in the 200–250°C range for plate work (verify with filler and section size).
-
Post-weld tempering or stress relieving is recommended to reduce brittleness.
-
For critical cosmetic surfaces, welding may require finishing/polishing testing to ensure consistency.
Quality Assurance and Mill Sources
-
Material supplied with heat numbers and mill test certificates.
-
Sourced from reputable mills, including brand equivalents such as BÖHLER M315 and other European/Japanese producers.
-
Optional higher cleanliness variants may be offered for improved consistency, depending on availability.
Industries Served
-
Plastic injection molders and mold makers
-
Aluminum die casting and pressure die casting tooling houses (bases, plates, fixtures)
-
Cutting tool and jig/fixture manufacturers
-
Automotive, appliance, and consumer goods mold shops
-
General engineering and fabrication for stainless tooling plates
Pricing in India
As a leading national supplier and importer, Milano Special Steel strives to offer the best price-to-performance ratio for DIN 1.2085 (AISI 420FM) in India. Final pricing depends on:
-
Dimensions and section thickness (saw yield and handling)
-
Quantity and frequency (spot vs. contract)
-
Brand/mill origin (standard vs. premium brands)
-
Condition (annealed vs. prehardened; additional processing)
-
Cleanliness and optional ESR-type variants (where applicable)
-
Delivery location and logistics
-
Market factors (exchange rates, freight, duties)
For the most competitive quote, share:
-
Grade and condition (e.g., DIN 1.2085 prehardened ~30–33 HRC)
-
Size list with tolerance and finish requirements
-
Quantity required (each size)
-
Delivery location and urgency
-
Any machining or value-added services needed (sawing, milling, grinding)
-
Alternative equivalent acceptance (e.g., BÖHLER M315 or other brand equivalents)
Tip for buyers: Consolidating sizes into optimized cut plans can reduce saw losses and improve overall project economics.
Delivery and Coverage
Our operational hubs are in Gurugram, Kundli, Sonipat, Manesar, Bawal, Bhiwadi, Dharuhera, Faridabad, Ghaziabad, Noida, and Greater Noida. We deliver to all Indian states and union territories, including Andhra Pradesh, Arunachal Pradesh, Assam, Bihar, Chhattisgarh, Goa, Gujarat, Haryana, Himachal Pradesh, Jharkhand, Karnataka, Kerala, Madhya Pradesh, Maharashtra, Manipur, Meghalaya, Mizoram, Nagaland, Odisha, Punjab, Rajasthan, Sikkim, Tamil Nadu, Telangana, Tripura, Uttar Pradesh, Uttarakhand, West Bengal, Andaman and Nicobar Islands, Chandigarh, Dadra and Nagar Haveli and Daman and Diu, Delhi, Jammu and Kashmir, Ladakh, Lakshadweep, and Puducherry, as well as major metro and industrial corridors such as Bangalore, Pune, and Surat.
Stock Programs and Services
-
Ex-stock plates and rounds for quick dispatch
-
Project-based reservations for large molds and toolroom schedules
-
Long-length saw cutting for batch kits
-
Rough and precision milling for setup-ready plates
-
Surface grinding to thickness/parallelism
-
Machining support and heat-treatment coordination
-
Customized packaging for safe interstate transport
Typical Use Scenarios
-
Mold base for PVC caps: 1.2085 in prehardened condition for base and support plates; 1.2316 for cavity cores facing corrosive gases; EDM for vent features; passivation before assembly.
-
Ejector plate renewals in humid environments: corrosion-resistant 1.2085 improves uptime compared to non-stainless plates; nitriding is selected for wear points to achieve extended life.
-
Pressure die casting fixture plates feature stainless backing plates and supports with stable pre-hardened hardness, minimizing rust from coolant splash and ambient humidity.
-
Toolroom universal stainless plates: general-purpose jig and fixture plates that machine quickly and maintain dimensional accuracy.
Technical Tips for Best Results
-
If the tool needs frequent wash-downs or runs corrosive plastics, select 1.2085 for base/frame components to reduce maintenance and rust marks.
-
For cavity blocks requiring a mirror finish, switch to 1.2083 or 1.2316, while retaining 1.2085 for plates to balance cost, machinability, and corrosion resistance.
-
Request stress relief after heavy roughing to minimize late-stage distortions.
-
Ensure proper toolpath planning and coolant flow during high-speed machining to maximize the benefits of free-machining sulfur while maintaining surface integrity.
-
For welded repairs, preheat, select proper filler, and temper/stress-relieve to maintain toughness around the weld zone.
Frequently Asked Questions (FAQs)
-
What is DIN 1.2085 Steel?
DIN 1.2085 Steel is a free-machining, stainless plastic mold steel with about 15–16% chromium and added sulfur for machinability. It is ideal for mold bases and plates that require corrosion resistance, consistent pre-hardened hardness, and fast machinability. -
Is DIN 1.2085 Steel the same as AISI 420?
No. AISI 420 (e.g., DIN 1.2083 type) generally exhibits higher polishability and may contain lower sulfur content. DIN 1.2085 Steel corresponds to AISI 420FM (free-machining variant) and is optimized for machining rather than ultimate mirror finish. -
Can I use 1.2085 for mirror-finish cavities?
It can achieve good finishes, but for the highest mirror gloss, 1.2083 or 1.2316 is often preferred. 1.2085 excels in bases, plates, and non-optical tooling. -
What hardness of DIN 1.2085 Steel is supplied?
Most customers select pre-hardened DIN 1.2085 Steel around 28–34 HRC (commonly around 30–33 HRC) for mold bases. Annealed material is available for custom heat treatment. -
Does DIN 1.2085 Steel corrode?
It is stainless and offers strong corrosion resistance compared to non-stainless tool steels. However, proper maintenance, passivation, and storage practices further enhance corrosion performance. -
Is welding possible?
Yes, with proper preheat, compatible fillers, and post-weld tempering or stress relief. -
How does it compare to P20?
DIN 1.2085 Steel offers better corrosion resistance and similar pre-hardened hardness, but generally has a higher cost than P20. Machinability is excellent due to the addition of sulfur. -
Is an ESR version available?
Some mills offer higher cleanliness or ESR-type variants. Availability depends on batch and sourcing; contact us for current options. -
Do you provide cut pieces and custom sizes?
Yes. We support both single-piece cut-to-size orders and bulk lists for production. -
Are MTCs provided?
Yes, mill test certificates are provided with heat and batch traceability.
Buyer’s Checklist for Quick Quotes
-
Grade: DIN 1.2085 Steel (X33CrS16, AISI 420FM)
-
Condition: Prehardened (target HRC) or annealed
-
Sizes: Thickness × Width × Length or Diameter × Length
-
Quantities: Per size
-
Tolerance: Cutting, finish, and flatness goals
-
Services: Sawing, milling, grinding, drilling
-
Delivery: Location and timeline
-
Alternatives: Acceptance of equivalent brands (e.g., BÖHLER M315)
Why DIN 1.2085 Steel Is a Smart Choice in India
-
Reduces downtime from rust and humidity on mold bases, especially in coastal and monsoon-prone regions.
-
Improves machining throughput thanks to sulfur additions—important for toolrooms with tight lead times.
-
Lowers total cost of ownership by reducing maintenance and increasing mold uptime.
-
Ideal for suppliers serving the automotive, consumer goods, appliance, and packaging industries, where mold productivity is critical.
Company Heritage and Capability
Established in 1972, Milano Special Steel has over five decades of experience in tool and mold steels. We are trusted by mold makers, automotive suppliers, die casters, and precision engineering firms across India. Our strengths include deep inventory, technical support, and reliable after-sales service. We help customers select the right grade—1.2085 for corrosion-resistant bases, 1.2083/1.2316 for mirror cavities, P20 for cost-effective general molds, and H13 for hot-work inserts—ensuring productivity and tool life.
Ordering and Logistics
-
Quick RFQ response with optimized cut plans
-
Flexible dispatch options, including same-day and next-day for stock items
-
Robust packaging to protect surfaces during transit
-
Coordination with your machine schedule to reduce bottlenecks
Summary of Advantages
-
Strong corrosion resistance for tooling plates and bases
-
Excellent machinability and chip control
-
Stable pre-hardened hardness for consistent performance
-
Broad availability in plates and rounds with cut-to-size service
-
Backed by mill test certificates and brand-equivalent options
Recommended Complementary Grades
-
1.2083 (AISI 420): High polishability for optical or high-gloss molds
-
1.2316: Superior corrosion resistance and good toughness for cavity blocks
-
P20/1.2311/1.2312: General-purpose plastic mold steel for non-corrosive applications
-
H13/1.2344 ESR: Hot-work and die-casting inserts where thermal fatigue resistance is critical
Ready-To-Use Package Options
-
Pre-squared and parallel-ground plates to reduce your setup time
-
Pre-drilled base plates for standard mold layouts (on request)
-
Matched sets for multi-plate assemblies
-
Passivated and protected surfaces to maintain corrosion resistance during storage
Environmental and Maintenance Tips
-
After running corrosive plastics, clean and dry plates before storage.
-
Use rust preventives and protective films for downtime periods.
-
Consider passivation to maximize corrosion resistance after heavy machining.
Final Note on Specifications
All technical data provided here is typical values and guidance-level information. Please refer to the mill test certificate and your process requirements for the exact parameters. For specialized applications, our technical team can assist with grade selection, heat treatment planning, and finishing strategies to optimize performance.