
Description
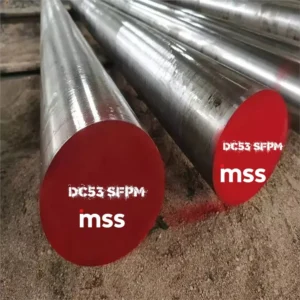
DC53 Steel High-Toughness Cold Work Tool Steel Best Price, Importer, and top Supplier in India
DC53 Steel is a modern, high-toughness, general-purpose cold work tool steel engineered as a significant upgrade over traditional D2 (JIS SKD11). By combining higher attainable hardness, refined carbide distribution, and superior purity, DC53 Steel delivers exceptional wear resistance, toughness, fatigue strength, and machining performance—exactly what precision dies, punching dies, and stepped punch applications demand in production environments.
At Milano Special Steel, we specialize in premium tool steels and mold steels for demanding Indian industries. With extensive stock in plates and rounds, precision cutting services, strict quality control, and fast country-wide delivery, we help manufacturers source DC53 Steel confidently and cost-effectively.
What Is DC53 Steel?
DC53 Steel is an advanced cold work tool steel designed to overcome the limitations of D2/SKD11. It achieves higher hardness—typically 62–64 HRC after high-temperature tempering—while offering roughly double the toughness of D2. Thanks to smaller, more uniformly distributed primary carbides and reduced non-metallic inclusions, DC53 maintains its edge longer, resists chipping, and exhibits better dimensional stability after heat treatment.
Key performance differentiators versus conventional D2/SKD11 include:
-
Higher usable hardness at high tempering temperatures for improved temper resistance.
-
Toughness levels suitable for fine punching of high-strength sheet, precision dies, and stepped punches.
-
Lower risk of early edge chipping and micro-cracking, improving tool life and consistency.
-
Better machinability and grindability contributing to shorter lead times and lower total cost per part.
For Indian manufacturers in automotive, white goods, electronics, fasteners, appliance components, and general engineering, DC53 Steel provides a robust, reliable platform for precision cold work tooling where durability and dimensional control matter.
DC53 Steel Typical Chemical Composition
The composition below is representative of DC53 Steel as supplied by leading producers. Values may vary slightly by melt and supplier, while staying within typical ranges.
| Element | Typical Range (%) |
|---|---|
| C | 0.95–1.05 |
| Si | 0.50–1.00 |
| Mn | 0.20–0.60 |
| Cr | 7.80–8.50 |
| Mo | 1.80–2.20 |
| V | 0.25–0.50 |
| P | ≤ 0.030 |
| S | ≤ 0.030 |
What this chemistry delivers:
-
Carbon and chromium provide the primary carbide-forming backbone for wear resistance.
-
Molybdenum raises secondary hardening response and temper resistance at high tempering temperatures.
-
Vanadium refines carbide size and distribution, enhancing wear resistance and toughness.
-
Silicon aids strength and temper resistance.
-
Controlled phosphorus and sulfur minimize inclusions, improving fatigue strength and polishability.
DC53 Steel Mechanical Properties and Hardness
-
Hardness after hardening and tempering: 62–64 HRC (with high-temperature tempering around 520–540°C).
-
Toughness: Approximately double that of conventional D2/SKD11 at comparable hardness, reducing chipping and extending die life.
-
Wear resistance: Very high due to refined carbide population and elevated hardness.
-
Fatigue strength: Enhanced by cleaner microstructure and refined carbides, improving resistance to micro-cracks and thermal fatigue.
-
Dimensional stability: Better than D2/SKD11 after heat treatment, improving accuracy for tight-tolerance dies and punches.
-
Annealed hardness (supply condition): Typically around 230–255 HB for machining.
These characteristics make DC53 Steel a preferred choice for precision punching of higher-strength steels, fine blanking, cold forming, and applications where D2/SKD11 struggles with chipping or premature edge breakdown.
DC53 Steel Heat Treatment Guidelines
Proper heat treatment is essential to realize DC53’s full performance. The following guidelines are commonly used in industry. Always adjust to section size, furnace uniformity, and specific application requirements.
-
Annealing (for machinability):
-
Heat to 800–850°C, hold to equalize, then furnace cool to 650°C at ≤ 10°C/h.
-
Air cool to room temperature. Target hardness: 230–255 HB.
-
-
Stress relieving (after heavy rough machining):
-
180–200°C for 1–2 hours, air cool.
-
-
Preheating:
-
Two-stage recommended: 550–600°C, then 850–900°C. This reduces thermal shock and helps uniform austenitization.
-
-
Austenitizing:
-
1020–1050°C. Hold time depends on section thickness (typical soak 20–30 minutes at temperature after achieving core temperature).
-
Use a protective atmosphere or a vacuum to reduce decarburization and scaling.
-
-
Quenching:
-
Options include warm oil quench, air/positive pressure gas quench, or salt bath with martempering.
-
For the best balance of hardness and low distortion, many users employ salt bath quench to 540–580°C with subsequent air cool.
-
-
Tempering:
-
Temper at high temperatures (typically 520–540°C) to achieve 62–64 HRC and excellent temper resistance.
-
Temper at least twice (2 hours each). A third temper may be used for critical dies.
-
Avoid tempering within lower ranges that can compromise toughness; DC53’s design favors high-temperature tempering for optimal performance.
-
-
Sub-zero treatment (optional):
-
Apply between quench and first temper at −70°C to −196°C for 1–3 hours to reduce retained austenite.
-
Follow with tempering cycles. Expect marginal hardness gain and improved dimensional stability.
-
-
Post-EDM temper:
-
After EDM, stress-relieve at approximately 180–200°C for 1–2 hours to reduce residual tensile stresses and avoid micro-cracks.
-
These steps—especially high-temperature tempering—are core to DC53’s advantage over D2/SKD11, enabling higher working hardness together with improved toughness.
DC53 Steel Machining, Grinding, EDM, and Polishing
-
Machinability:
-
DC53 Steel machines are superior to D2 due to their refined carbides and improved cleanliness.
-
Use rigid setups and sharp carbide tooling; apply flood coolant to control heat.
-
Recommended practice is to leave sufficient stock for grind and heat-treat movement (typical allowance 0.15–0.30% per dimension, depending on section).
-
-
Grinding:
-
Use soft-grade, open-structure wheels suitable for hardened tool steels.
-
Control heat; avoid grinding burn. Dress wheels frequently and employ abundant coolant.
-
For precision surfaces, employ incremental passes and spark-out to minimize residual stresses.
-
-
EDM/Wire Cutting:
-
DC53 Steel shows lower susceptibility to EDM micro-cracking than D2/SKD11.
-
Use fine-finish settings for final passes. After EDM, stress-relieve at ~180–200°C for 1–2 hours.
-
-
Polishing:
-
Enhanced purity makes DC53 Steel responsive to high-quality polish, suitable for precision die surfaces and wear inserts.
-
Use progressive abrasives and keep the surface free of embedded debris.
-
-
Weld repair:
-
Preheat to 200–250°C to mitigate cracking. Use a compatible filler.
-
Post-weld temper or stress-relieve to restore toughness and reduce residual stress. For critical tools, plan a full re-temper cycle.
-
DC53 Steel Surface Engineering and Coatings
Surface treatments further extend tool life and performance in severe service.
-
Nitriding and nitrocarburizing:
-
Typical nitriding temperatures: 500–520°C.
-
Case hardness: up to approximately 1000–1200 HV, with case depths tailored to requirement (for example, 0.15–0.40 mm).
-
Nitriding is effective for sliding wear and galling reduction on punches and dies.
-
-
PVD coatings:
-
TiN, TiCN, AlTiN, CrN, and DLC coatings reduce friction, increase surface hardness, and resist adhesive wear.
-
PVD is preferred for DC53 Steel due to low process temperatures (< 500°C), preserving core hardness.
-
-
Duplex treatments (nitriding + PVD):
-
Combining nitriding with PVD yields high load-carrying compound layers and low-friction topcoats, ideal for fine blanking and high-strength sheet punching.
-
-
Ion/plasma nitriding:
-
Offers precise control of compound layer formation and minimizes distortion on precision tools.
-
Selecting the right surface treatment depends on the wear mechanism (abrasive, adhesive, or fatigue), sheet material, lubrication, and production volume.
Applications of DC53 Steel
DC53 Steel thrives where toughness and wear resistance must coexist at high working hardness. Common applications include:
-
Precision punching dies and stepped punches for high-strength steels and stainless sheets.
-
Fine blanking dies demanding clean edges and minimal chipping.
-
Cold forming dies, bending dies, and drawing dies where edge stability is critical.
-
Shear blades, trimmer blades, and slitter knives for tighter tolerances and longer campaigns.
-
Cold extrusion dies, thread rolling dies, and roll forming tool components.
-
Wear inserts, guide rails, wear plates, and bushings in tooling systems.
-
Gauges and fixtures requiring dimensional stability and polishability.
Alongside DC53 for cold work, Milano Special Steel also supports allied industries such as aluminum die casting, pressure die casting, plastic mold production, sheet metal cutting, cutting tool manufacturing, automotive components, and forging by supplying appropriate hot work and mold steels for those applications.
DC53 Steel vs Alternatives
Selecting the right steel depends on sheet material, thickness, load case, and tool life targets. The table below compares DC53 Steel with commonly considered grades.
| Property | DC53 Steel | D2 (AISI) | JIS SKD11 | A2 (AISI) | H13 (AISI) |
|---|---|---|---|---|---|
| Type | High-toughness cold work | High-carbon, high-chromium cold work | JIS D2-equivalent cold work | Air-hardening cold work | Hot work tool steel |
| Typical Hardness | 62–64 HRC (high-temp temper) | 58–62 HRC | 58–62 HRC | 57–60 HRC | 44–52 HRC |
| Toughness | Higher (≈2× D2) | Moderate | Moderate | Higher than D2, lower wear | High at lower hardness |
| Wear Resistance | Very high | Very high | Very high | Moderate–high | Moderate |
| Temper Resistance | Excellent at 520–540°C | Moderate | Moderate | Moderate | Excellent for hot work |
| Dimensional Stability | Very good | Good | Good | Good | Good |
| Machinability | Better than D2 | Fair | Fair | Good | Good |
| Primary Use | Precision cold work dies/punches | General cold work | General cold work (JIS) | General cold work with more toughness | Hot work (die casting/forging) |
Key takeaways:
-
Choose DC53 Steel when edge chipping is limiting tool life with D2/SKD11 and when higher working hardness is needed without sacrificing toughness.
-
Choose A2 if shock loading dominates and the wear environment is less severe.
-
Choose H13 for hot work (die casting, forging); it is not a cold work steel and operates at different hardness and temperature regimes.
DC53 Steel Stock, Sizes, and Forms at Milano Special Steel
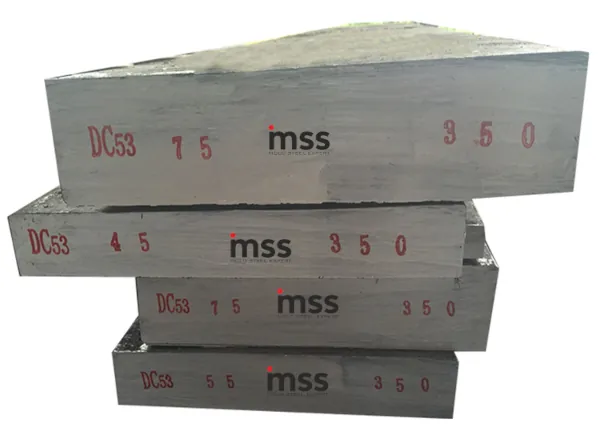
Milano Special Steel supplies DC53 Steel in both plate and round bar, with robust inventory for quick turnarounds and cut-to-size services.
-
Forms:
-
Precision-sawn plates, milled flats, and ground plates upon request.
-
Hot-rolled and forged rounds, peeled/turned rounds on request.
-
Near-net cut pieces for punches, inserts, and die blocks.
-
-
Typical size range:
-
Plates: from thin sections for small dies to thick blocks suitable for large tools.
-
Rounds: small diameters for punches to larger diameters for extrusion and forming dies.
-
-
Custom cutting:
-
CNC band saw and plate saw capacity for tight-tolerance blanks.
-
Nesting optimization to minimize scrap and lower the cost per piece.
-
-
Value-added:
-
Normalizing/annealing services when required for special machining sequences.
-
UT-tested blocks for critical applications.
-
Rough and finish machining partnerships available on request.
-
Quality Assurance and Documentation
To support consistent, repeatable tooling performance, Milano Special Steel emphasizes certification and testing.
-
Mill Test Certificates (MTC) as per EN 10204 (typically 3.1).
-
Heat/lot traceability for every piece.
-
Ultrasonic testing (UT) is performed to recognized standards for internal soundness.
-
Dimensional inspection reports for cut-to-size parts.
-
Hardness verification and microcleanliness records where applicable.
-
Packaging for corrosion protection and safe transport.
The combination of documented quality and material consistency reduces process variability and total lifecycle cost for dies and punches.
Industries and Use Cases We Serve
We cater to wholesale and retail customers across:
-
Precision sheet metal cutting and progressive die shops.
-
Tier-1 and Tier-2 automotive component manufacturers.
-
Appliance and white goods producers.
-
Electrical and electronics stamping suppliers.
-
Cutting tool manufacturers and general engineering.
-
Plastic mold makers need wear inserts and sliding components.
-
Forging and die casting companies for trimming dies and ancillary cold work tools.
Whether you need one-off development blanks or high-volume repeat orders, our team aligns stock availability, cutting, and logistics with your production schedule.
Pan-India Delivery Footprint
With over 50 years of industry experience (established in 1972), Milano Special Steel operates from key hubs in Gurugram, Kundli, Sonipat, Manesar, Bawal, Bhiwadi, Dharuhera, Faridabad, Ghaziabad, Noida, Greater Noida, and the RIICO industrial regions, delivering DC53 Steel across India, including:
-
Andhra Pradesh
-
Arunachal Pradesh
-
Assam
-
Bihar
-
Chhattisgarh
-
Goa
-
Gujarat
-
Haryana
-
Himachal Pradesh
-
Jharkhand
-
Karnataka
-
Kerala
-
Madhya Pradesh
-
Maharashtra
-
Manipur
-
Meghalaya
-
Mizoram
-
Nagaland
-
Odisha
-
Punjab
-
Rajasthan
-
Sikkim
-
Tamil Nadu
-
Telangana
-
Tripura
-
Uttar Pradesh
-
Uttarakhand
-
West Bengal
-
Andaman and Nicobar Islands
-
Chandigarh
-
Dadra and Nagar Haveli and Daman and Diu
-
Delhi
-
Jammu and Kashmir
-
Ladakh
-
Lakshadweep
-
Puducherry
-
Bangalore
-
Pune
-
Surat
Our logistics team plans dispatches to meet your shutdown, PPAP, and SOP timelines, balancing cost and speed with reliable packaging and tracking.
How to Choose DC53 Steel vs Other Grades
Use the decision points below to select DC53 Steel with confidence:
-
If your D2/SKD11 punch tips chip prematurely, migrate to DC53 for higher toughness at the same or higher hardness.
-
If you require 62–64 HRC after high-temperature tempering for superior temper resistance, DC53 is the better option.
-
For very high shock loads with moderate wear, consider A2; for hot work at elevated temperatures, consider H13 or equivalent.
-
For ultra-high wear (abrasive) with limited shock, powder metallurgy grades may be evaluated—but DC53 often offers a more economical balance for production punching and forming.
-
If tight tolerances after heat treatment are critical, DC53’s dimensional stability gives it an edge over conventional D2/SKD11.
Practical Tips for Toolmakers and Production Engineers
-
Stock removal strategy:
-
Rough machine, stress-relieve, finish machine, then heat treat for consistent geometry.
-
-
Heat treat fixturing:
-
Support thin sections to reduce distortion; use vacuum hardening where available for clean surfaces and minimal scale.
-
-
Edge preparation:
-
Micro-chamfers or edge honing can significantly improve the life of high-strength sheet.
-
-
Lubrication:
-
Optimize lubricant selection and delivery; DC53 responds well to improved lubrication in adhesive wear regimes.
-
-
Coating selection:
-
Match PVD coating to sheet material: for example, AlTiN/AlCrN for abrasive wear, DLC/CrN for lower friction with stainless and galvanized substrate.
-
-
Maintenance:
-
Regular regrinds maintain geometry and prevent catastrophic failures; DC53’s toughness helps extend intervals between maintenance cycles.
-
DC53 Steel Price, Availability, and Ordering
We maintain strong inventory positions to offer competitive pricing and dependable lead times for DC53 Steel plates and rounds. Pricing depends on section size, quantity, UT requirements, finish condition, and cutting complexity. To expedite a quote:
-
Share required dimensions, tolerances, and plan view/drawings for cut pieces.
-
Indicate the hardness specification and whether heat treatment will be performed in-house or supplied.
-
Specify UT levels, MTC/QA documentation, and any surface preparation or coating needs.
-
Provide delivery location and target date to optimize freight options.
Our team will respond with the best available price, stock status, and delivery window, aligning with your project’s critical path.
Frequently Asked Questions (FAQs)
-
What is DC53 Steel used for?
-
DC53 is used for precision cold work tooling such as punches, dies, fine blanking tools, cold forming and drawing dies, shear blades, and wear components where high hardness and toughness are required.
-
-
Is DC53 the same as D2 or SKD11?
-
No. While related to the D2/SKD11 family, DC53 is an improved grade with refined carbides and alloy adjustments that deliver higher hardness at high tempering temperatures and significantly greater toughness.
-
-
What hardness can I expect after heat treatment?
-
With proper heat treatment and high-temperature tempering (around 520–540°C), expect 62–64 HRC.
-
-
Do I need cryogenic treatment?
-
Sub-zero treatment is optional. It can reduce retained austenite and improve stability, which is valuable for tight tolerances or very high wear demands.
-
-
Can DC53 be nitrided or coated?
-
Yes. DC53 responds very well to nitriding/nitrocarburizing and to PVD coatings like TiN, AlTiN, CrN, and DLC. Duplex nitriding + PVD is often used for demanding punching and fine blanking.
-
-
How does DC53 perform after EDM?
-
Better than D2/SKD11, with reduced risk of micro-cracking. Nonetheless, always apply a low-temperature stress-relief after EDM.
-
-
What about polishability?
-
DC53’s high purity and refined carbides allow good polishing, suitable for critical die surfaces and wear inserts.
-
-
What is the annealed hardness for machining?
-
Typically around 230–255 HB in the annealed delivery condition.
-
-
Does Milano Special Steel supply cut-to-size blanks?
-
Yes. We provide precision-sawn blanks and near-net shapes in plates and rounds, optimized to your drawings.
-
-
Do you deliver across India?
-
Yes. We service all Indian states and union territories with dependable logistics from our North India hubs.
-
Why Milano Special Steel for DC53 Steel
-
Over five decades of expertise: Established in 1972 with a legacy of serving India’s tool and die ecosystem.
-
Comprehensive product portfolio: DC53 Steel alongside D2/SKD11, H13, A2, and other premium grades for cold work, hot work, and plastic molds.
-
Strong inventories: Plates and rounds in a wide range of dimensions for urgent and scheduled requirements.
-
Precision services: Cut-to-size, UT-tested stock, MTC documentation, and tailored packaging.
-
Competitive pricing: Value-engineered quotes that reduce the total cost of ownership for tooling.
-
Technical support: Practical, shop-floor-centric guidance on grade selection, heat treatment, and surface engineering.
Summary for Buyers and Engineers
If your application demands high hardness with superior toughness, reduced chipping, and longer tool life than D2/SKD11 typically provides, DC53 Steel is the right choice. It streamlines toolroom work, boosts die reliability in production, and helps meet tighter tolerances under challenging conditions. Milano Special Steel backs that material advantage with quality documentation, fast cutting services, and pan-India delivery—so your dies and punches start strong and stay in spec longer.